
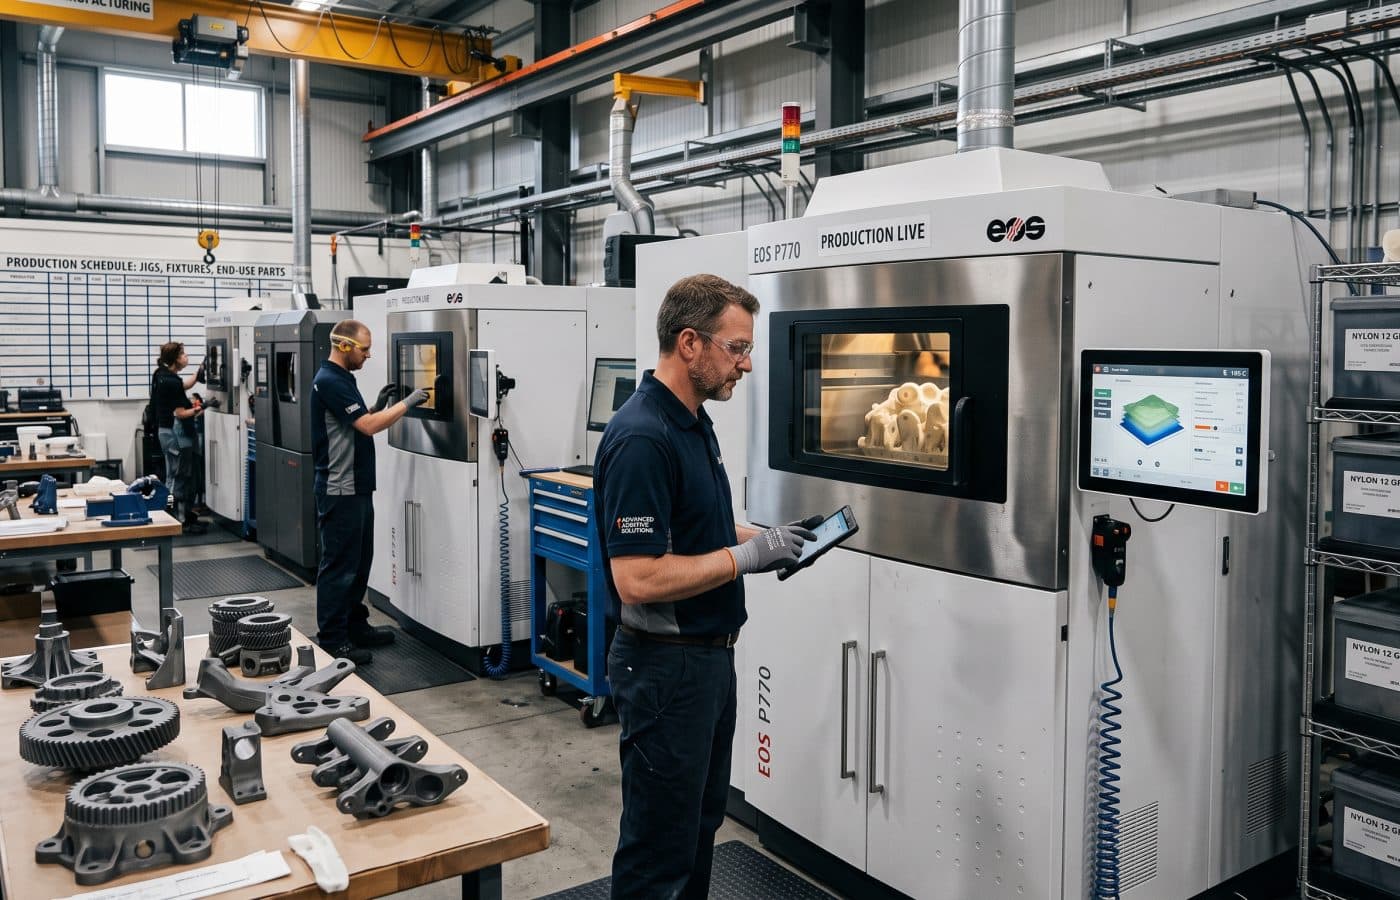
Industrial 3D Printing: How Manufacturers Are Using It Beyond Prototypes

The first industrial 3D printing job I ever signed off for a production line was not glamorous. In fact, it was a gripper finger for a pick and place cell, printed in stainless steel. It replaced a machined assembly of four pieces that kept working loose on the night shift. As a result, nobody outside the maintenance crew ever noticed it, and that was the whole point.
I bring it up because most people still picture industrial 3D printing as the machine in the corner of the R&D lab that makes plastic models for design reviews. That picture was fair fifteen years ago. Today, however, it is badly out of date. In my work as an additive manufacturing engineer, the part of the job that has grown the most has very little to do with prototypes. Instead, it is tooling, spare parts, repairs, and real production components that end up inside products people buy.
This article walks through how manufacturers actually use industrial 3D printing today. First, it covers where the technology pays off. Then it looks at where it quietly fails, and finally at what I tell plant managers who ask where to start. Throughout, I lean on published case data from companies that have done this at scale, because numbers persuade better than enthusiasm.
Why the Prototype Label No Longer Fits Industrial 3D Printing
Prototyping built this industry, and it still matters. Even so, the money has moved.
What the Industrial 3D Printing Market Numbers Say
According to Wohlers Report 2026, global additive manufacturing revenue reached $24.2 billion in 2025, up 10.9% on the year before. However, the more telling detail sits underneath that headline. Manufacturing services held the largest share of the market at 48%. In addition, services grew 15.5% while machine sales grew only 3.6% (Metal AM).
Read that the way an engineer would. In other words, companies are not mainly buying printers to sit in a lab. Instead, they are paying for parts, and for the know how to qualify those parts. Accordingly, Wohlers frames it as a maturing industry where value is shifting toward production and service delivery rather than new hardware.
Similarly, forecasters heading into 2026 said the same thing more bluntly. They said the year would be judged on industrial parts produced, machine utilization, and measurable return on investment, not on how many printers got sold (3D Printing Industry).
That matches what I see on shop floors. Years ago, the question was “can we print it?” Now, by contrast, it is “can we print it repeatably, at a cost per part that beats the alternative, and will quality sign off on it?”
A Quick Note on Terms
Industrial 3D printing and additive manufacturing (AM) mean the same thing in practice. Specifically, the ISO/ASTM 52900 standard sorts every AM process into seven families (PADT):
- binder jetting
- directed energy deposition
- material extrusion
- material jetting
- powder bed fusion
- sheet lamination
- vat photopolymerization
Therefore, every process I mention below fits in one of those buckets.
1. Industrial 3D Printing for Jigs, Fixtures, and Shop Floor Tooling
If I could recommend only one starting point, it would be this. Jigs, fixtures, gauges, and assembly aids are the plain tools that hold, locate, and check parts on a line. Usually, they are one of a kind, and they change whenever the product changes. Traditionally, an outside shop machines them with lead times measured in weeks.
The Volkswagen Autoeuropa Example
Volkswagen Autoeuropa in Portugal is the case everyone cites, and for good reason. To begin with, the plant validated the idea in 2014. After that, it went on to produce 93% of its previously outsourced tools in house on a handful of desktop extrusion printers.
For example, one liftgate badge tool used to take 35 days and cost €400 from a supplier. Printed in house, however, it took 4 days and cost about €10 per part. Overall, the plant reported a 91% cut in tool development cost and 95% less development time (UltiMaker). Likewise, a wheel protection jig that used to cost up to €800 per part is now printed for a small fraction of that (TCT Magazine).
Why Operators Matter as Much as Savings
What the headline numbers miss, though, is the operator side. When a fixture costs €20 and prints overnight, the person using it can ask for a change on Tuesday and test it Wednesday. Over time, I have watched assembly techs go from tolerating awkward tools to actively redesigning them with us. As a result, that feedback loop is worth as much as the savings.
That is exactly why I push tooling first. It is low risk, it pays back fast, and, above all, it builds internal skill before you touch anything safety critical.
A Practical Tip on Materials
Here is one tip from experience. To start, print fixtures in a tough engineering material such as nylon or a carbon filled grade, not the cheapest filament on the shelf. Next, put threaded metal inserts where screws go. Finally, add a soft contact pad wherever the fixture touches a painted or machined surface. Those small details decide whether a printed fixture lasts a week or three years.
2. Injection Mold Inserts With Conformal Cooling
This one sits in metal powder bed fusion territory. Moreover, it is where I have seen some of the fastest payback on expensive machines.
How Conformal Cooling Works
In injection molding, cooling usually eats the biggest slice of each cycle. Conventional cooling channels, however, are gun drilled in straight lines, so they cannot follow a curved cavity. A printed mold insert, on the other hand, can carry channels that wrap around the shape of the part. That is what conformal cooling means.
The Results in Real Plants
The results are measurable, for instance:
- Bastech printed a conformally cooled insert that cut injection molding cycle time by 22%. It also removed 30 to 40 hours of mold post processing (Cimatron).
- Star Rapid reported a case where a printed core reduced cooling time by 38 seconds, roughly 60%, while also improving part quality (Star Rapid).
After all, cycle time is money on a molding line. If you take a few seconds off a part that runs hundreds of thousands of times a year, then the printed insert pays for itself quickly.
The catch, however, is design skill. For example, channels placed too close to the cavity wall, or too narrow to clean, will crack or clog. For this reason, model the thermal behavior before you print. In addition, plan how the channels will be flushed and inspected over the life of the tool.
3. Spare Parts and the Digital Warehouse
Maintenance managers understand this use case faster than anyone, because they live with the pain. Typically, an old machine breaks, and the original supplier no longer makes the part. Meanwhile, the line sits idle while purchasing hunts for an answer.
How Deutsche Bahn Built a Spare Parts Program
Deutsche Bahn turned that problem into a program. Initially, the German railway started in 2015 with simple parts like a plastic coat hook. Ten years later, it had produced more than 200,000 printed parts for more than 1,000 applications and saved more than 20 million euros (VoxelMatters).
One example is a gear housing for shunting locomotives. Through normal procurement, it took about ten months to arrive. Cast in a printed mold, by comparison, it took two (VoxelMatters). To do this, DB reverse engineers parts with 3D scanning. Then it either prints the part directly or prints the mold used to cast it (Deutsche Bahn).
The Record Behind the File
The idea underneath is the digital warehouse. In short, instead of shelves of physical stock, you store a validated file and a print recipe.
I like this model. Still, I always warn teams about one thing. The file is the easy part. The hard part, by contrast, is the record behind it: material, process parameters, inspection criteria, and who approved it. Without that, a digital warehouse is just a folder of STL files nobody trusts. Link each printable spare to its asset in your CMMS so technicians can find it when a machine goes down. And because those files are now production assets, store them on a network protected by proper OT cybersecurity controls.
4. Repair and Remanufacturing
Directed energy deposition and powder bed fusion can add material back onto worn components. Consequently, for expensive parts that run hot or wear hard, this is often the most valuable thing AM does.
The Siemens Energy Burner Repair
Siemens Energy’s work on gas turbine burners shows why:
- Conventional repair: technicians cut back about 120 mm of a damaged burner. They then replaced the burner pipe along with its fuel lines.
- Laser melting repair: only about 20 mm of the tip is removed and rebuilt. As a result, repair lead time dropped by about 90% (Laser Focus World).
EOS supplied the machine. Notably, it points out that the process also let Siemens upgrade older burner designs during the repair, instead of simply restoring them (EOS).
Repairs That Improve the Original
That last point is underrated. In effect, a repair becomes a chance to put an improved design into an old asset. In the plants I support, for example, the repair conversation usually starts with “how do we fix this faster.” Eventually, though, it ends with “can we make it outlast the original.”
5. Part Consolidation in Production Components
This is the use most people link with aerospace. Above all, the textbook case is GE’s fuel nozzle tip for the CFM LEAP engine.
The GE LEAP Fuel Nozzle
The earlier design was about 20 separate pieces brazed and welded together. Printed as one piece in a nickel alloy, however, it came out about 25% lighter and roughly five times more durable (VoxelMatters). Subsequently, GE’s plant in Auburn, Alabama began producing the tips in 2015 and later shipped its 100,000th one (Manufactur3D).
GE engineers have also been candid about what production really demands. Small tweaks are fine during development. Once a part enters production, however, the whole process has to be locked down (GE Aerospace).
That is the lesson I repeat most. Put simply, consolidation is a design win, but production is a process discipline.
Consolidation in Everyday Equipment
Of course, you do not need a jet engine to benefit. For instance, I have consolidated manifolds, brackets, and gripper assemblies for ordinary industrial equipment. Every joint you delete means:
- one less leak path
- one less fastener to torque
- one less line on the bill of materials in your ERP
- one less thing for the night shift to chase
6. Low Volume and Bridge Production With Industrial 3D Printing
Hard tooling for molding or die casting can take weeks and cost a lot before the first good part comes off. Fortunately, production grade polymer processes such as Multi Jet Fusion and selective laser sintering can fill that gap. Manufacturers use them, for example, to:
- launch a product before the hard tool is ready
- cover a supply disruption
- run variants that will never reach molding volumes
Why Demand Is Growing
Forecasters expect polymer AM to take a bigger role in tooling, service parts, and end use components (3D Printing Industry). Supply chain strain is also part of the push, since printing lets companies make parts closer to where the final product is assembled (Advanced Manufacturing).
Running the Cost Comparison
The math is simple, even when the inputs are not. Basically, you compare two numbers:
- the full cost per printed part, including post processing and inspection
- the hard tool cost spread over your realistic volume
For complex parts at a few thousand units a year, printing often wins. For simple parts at high volume, on the other hand, molding almost always wins.
The mistake I see most, however, is comparing machine time alone. People forget post processing, which can quietly become the largest line on the quote.
What Still Holds Industrial 3D Printing Back
I would be doing you a disservice if I made this sound easy. In reality, four issues come up on almost every project I touch.
Four Common Barriers
Qualification. A printed part is only as trustworthy as the process that made it. For example, powder lot, machine calibration, build orientation, heat treatment, and inspection all shape the result. Regulated industries therefore need documented, repeatable processes, and building that record takes months, not days.
Post processing. This covers support removal, stress relief, machining of critical faces, surface finishing, and clearing powder out of internal channels. Too often, people budget for the print and then get surprised by everything that comes after it.
Cost per part. Unlike molding, printing does not get cheaper with volume. So if your part is simple and you need a million of them, AM is the wrong tool. No amount of enthusiasm changes that.
People. Designing for additive is a different skill from designing for machining. Consequently, engineers trained on subtractive rules tend to print parts that look like machined parts. They then end up with machined part performance at printed part prices. For that reason, training and a few early, low risk wins matter more than buying the biggest machine on the market.
A Signal From the Market
There is also a market signal hidden in all this. In 2024, Wohlers found that revenue for machine makers declined, while materials suppliers posted the fastest growth (Metal AM). My reading, then, is that companies are running the machines they already own harder and buying more material to feed them. Ultimately, that is what a production oriented industry looks like.
How to Start With Industrial 3D Printing
- Walk the floor, not the catalog. First, list the fixtures, gauges, and spare parts that cause delays or cost too much. Your first applications are already sitting on the shop floor.
- Pick one low risk win. Next, choose a fixture or a non critical spare part. Then prove the full workflow: design, print, post process, inspect, approve.
- Write the recipe down. Record the material, machine, parameters, orientation, finishing steps, and acceptance criteria, ideally in your MES so every build is traceable. Later, this record becomes the foundation for everything you scale.
- Decide what to own and what to outsource. Polymer printers for tooling are cheap enough to own. Metal production, however, often makes more sense through a qualified service bureau at first. That also fits with services being the biggest slice of the AM market.
- Redesign, do not copy. Once the basics work, hunt for assemblies you can consolidate and parts you can lighten. After all, that is where the bigger returns live.
- Measure everything. Finally, track lead time, cost per part, downtime avoided, and scrap rate. Numbers keep the program funded when budgets tighten.
Final Thoughts on Industrial 3D Printing
Industrial 3D printing stopped being just a prototype tool a while ago. Today, the manufacturers getting real value from it use it for quiet, practical work:
- fixtures that cost a tenth of what they used to
- mold inserts that take seconds off every cycle
- spare parts that arrive in weeks instead of months
- repairs that return old assets better than new
- consolidated parts that simplify whole assemblies
None of that happens by buying a printer and waiting, however. Rather, it happens through process discipline, honest cost comparisons, and engineers who learn to design for the process instead of around it.
In short, start small, write everything down, and let the results argue for the next investment. That is how every successful AM program I have worked on got built.
Frequently Asked Questions About Industrial 3D Printing
What is industrial 3D printing used for besides prototypes?
The biggest uses today are:
- jigs and fixtures
- injection mold inserts with conformal cooling
- spare parts on demand
- repair of worn components
- consolidated production parts
- bridge production before hard tooling is ready
For example, Volkswagen Autoeuropa and Deutsche Bahn are two well documented cases (ultimaker.com, deutschebahn.com).
How big is the industrial 3D printing market?
Wohlers Report 2026 puts global additive manufacturing revenue at $24.2 billion for 2025. In addition, manufacturing services take the largest share (metal-am.com).
Is industrial 3D printing cheaper than injection molding?
It depends on volume and complexity. Because printing avoids tooling cost, it often wins for complex parts in low volumes. For simple parts at high volume, however, molding is usually cheaper per part. Either way, always include post processing and inspection in the comparison.
Which industrial 3D printing processes are used for production parts?
For metal, laser powder bed fusion and directed energy deposition are the most common. For polymers, meanwhile, Multi Jet Fusion, selective laser sintering, and engineering grade material extrusion lead. All of them fall within the seven process families defined by ISO/ASTM 52900 (padtinc.com).
Can 3D printed parts be certified for critical applications?
Yes, as long as the full process is controlled and documented. For instance, GE’s printed LEAP fuel nozzle tip flies in commercial jet engines. Even so, GE stresses that production processes must be locked down once qualified (geaerospace.com).
What is the easiest way to start with industrial 3D printing?
Start with jigs and fixtures. They are low risk and pay back quickly. More importantly, they teach your team the full workflow before you move on to spare parts or production components.
References
- Metal AM. New Wohlers Report 2026 highlights $24.2B global Additive Manufacturing market. metal-am.com
- Metal AM. Wohlers Report 2025 shows global Additive Manufacturing industry growth over 9%. metal-am.com
- 3D Printing Industry. The Future of 3D Printing: Additive Manufacturing Expert Forecasts for 2026. 3dprintingindustry.com
- PADT. Definition: ASTM Additive Manufacturing Processes. padtinc.com
- UltiMaker. Volkswagen Autoeuropa: Maximizing production efficiency with 3D printed tools, jigs, and fixtures. ultimaker.com
- TCT Magazine. Can you jig it? 3D printing inside Volkswagen Autoeuropa. tctmagazine.com
- Cimatron. Bastech Uses 3D Printed Conformal Cooling Inserts to Reduce Costs and Time. cimatron.com
- Star Rapid. Metal 3D Printing for Conformally Cooled Injection Molds. starrapid.com
- VoxelMatters. Deutsche Bahn celebrates 10 years of 3D printing. voxelmatters.com
- VoxelMatters. Deutsche Bahn (DB) 3D prints 100,000th part. voxelmatters.com
- Deutsche Bahn. Printing in progress: DB at work. deutschebahn.com
- Laser Focus World. Status of additive manufacturing for gas turbine components. laserfocusworld.com
- EOS. 3D Printing for High Performance Industrial Gas Turbines (Siemens case study). eos.info
- VoxelMatters. How Greg Morris created the 3D printed nozzle for GE’s LEAP engine. voxelmatters.com
- Manufactur3D. GE Aviation Produced Its 100,000th 3D Printed Fuel Nozzle Tip. manufactur3dmag.com
- GE Aerospace. The devil is in the details: So, you 3D printed a part for a jet engine. Now what? geaerospace.com
- Advanced Manufacturing. Driving a New 3D Printing Dynamic in 2026. advancedmanufacturing.org