 By Robert Smith
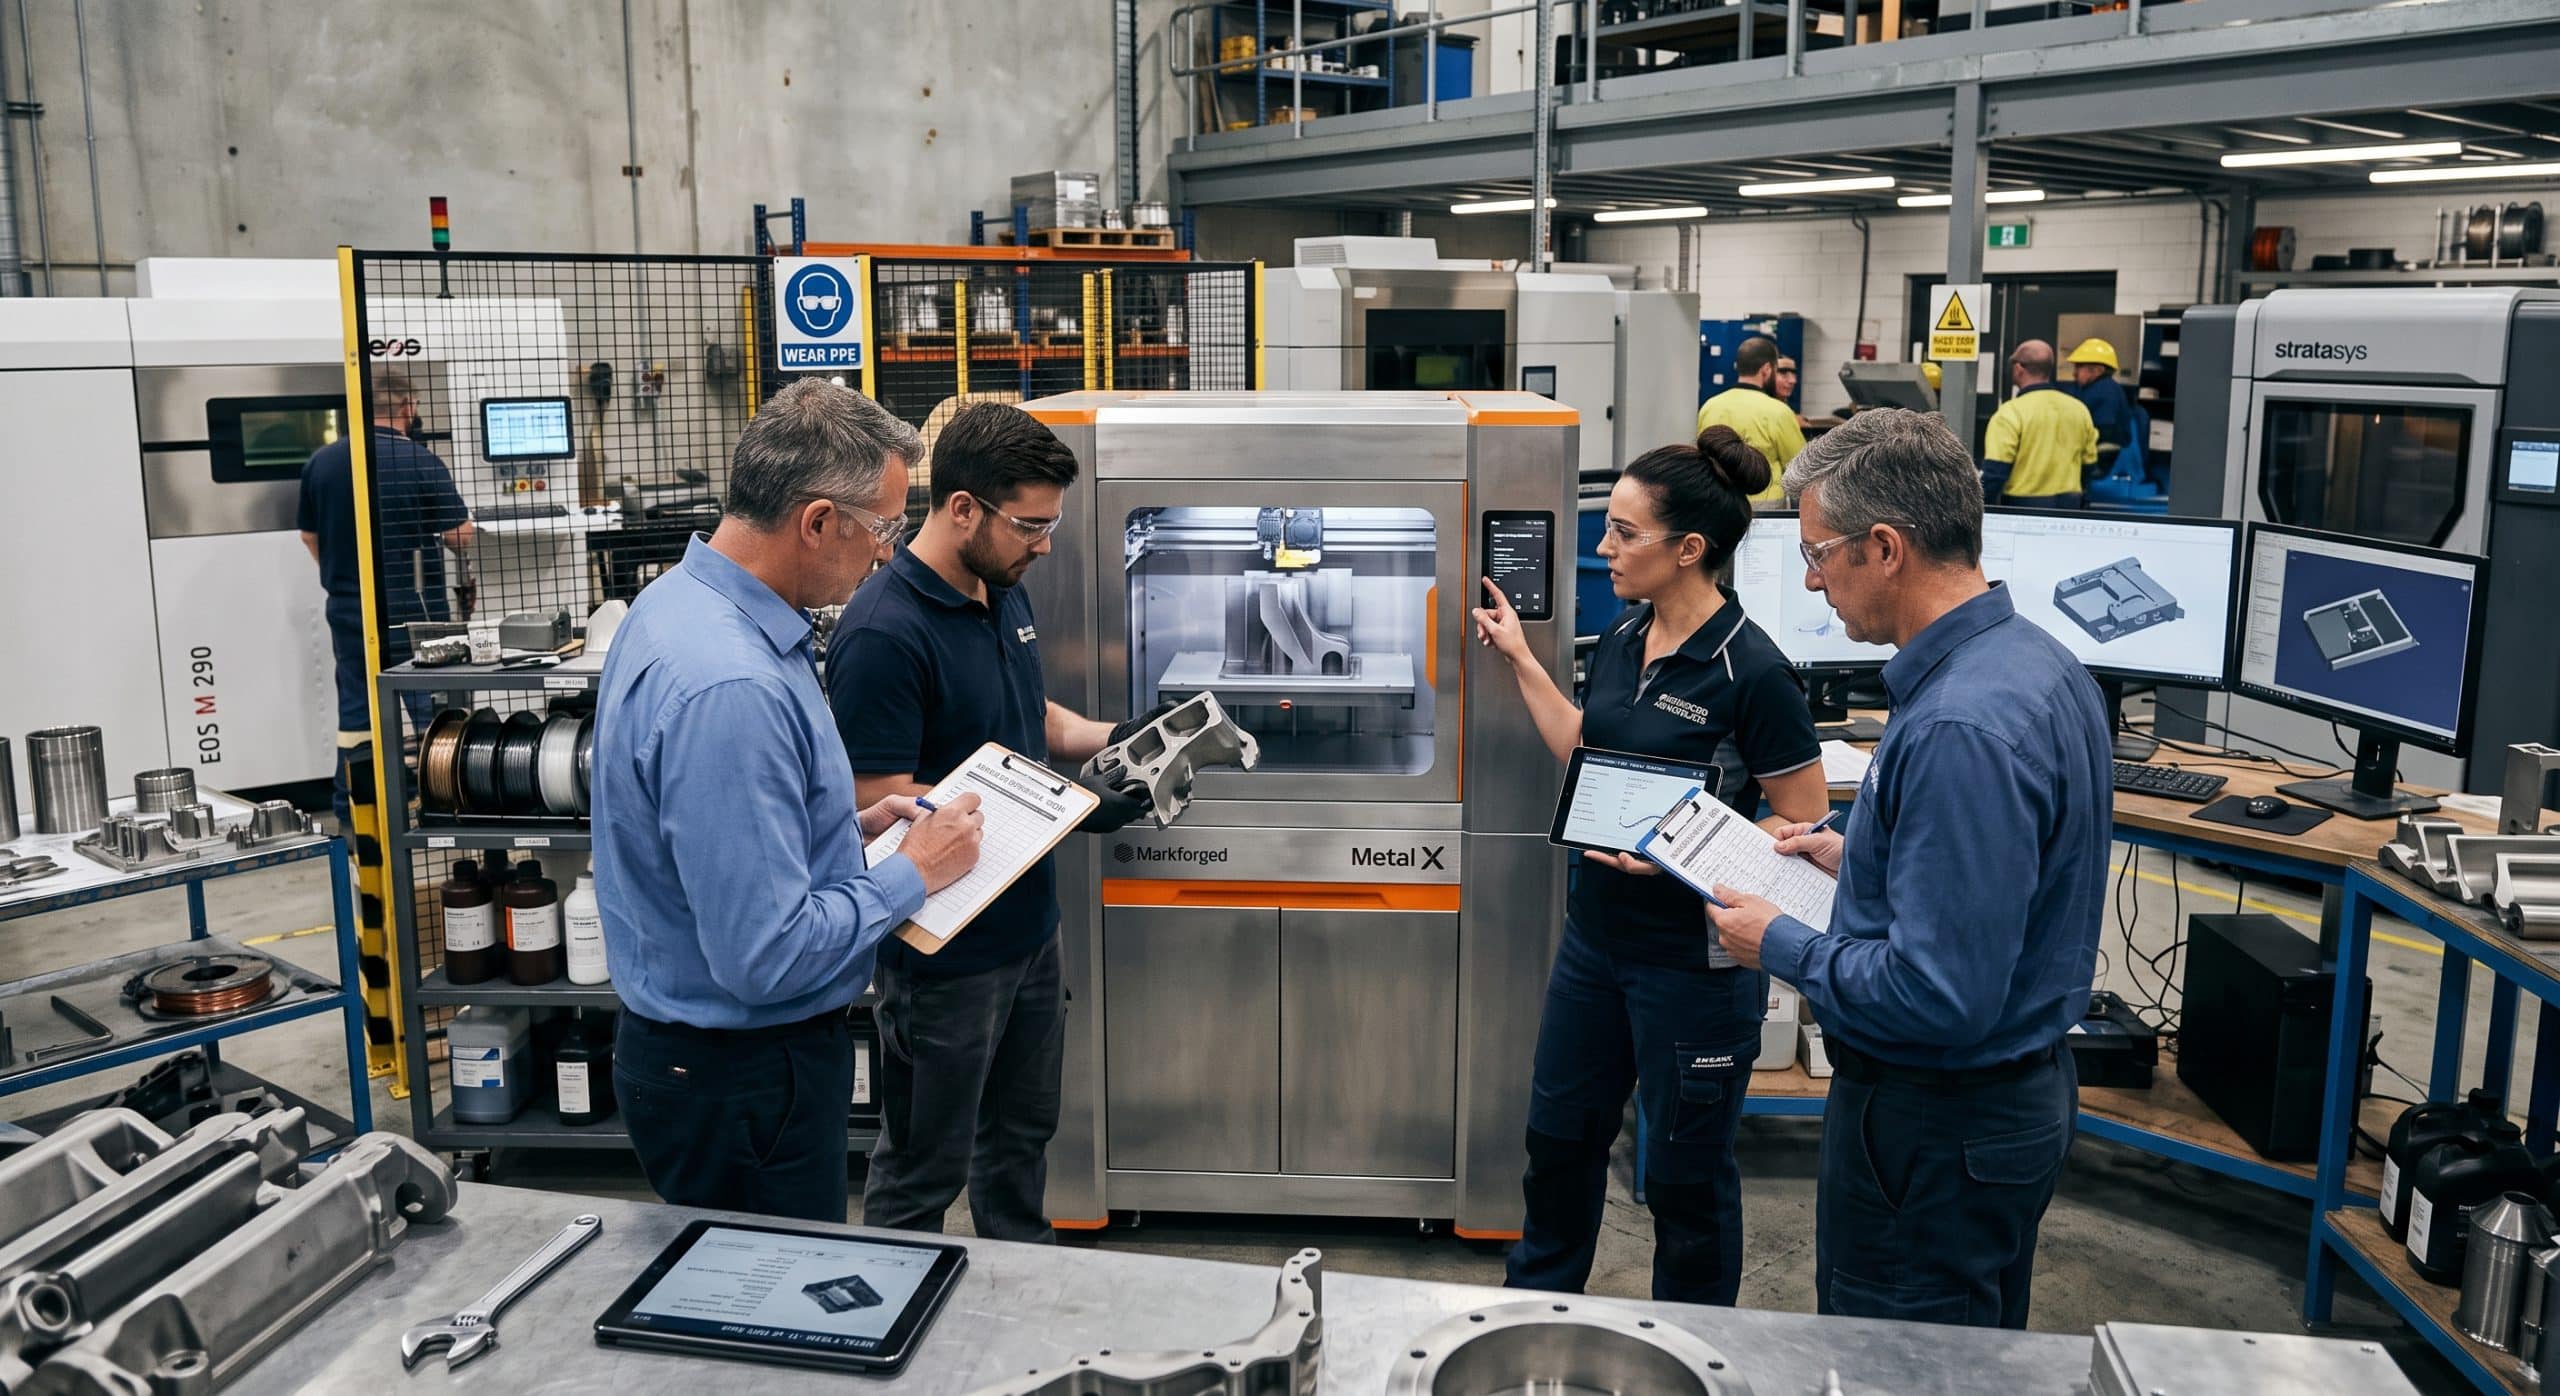
I have lost count of how many times a plant manager has walked me over to an empty corner of the shop floor, pointed at it, and said, “We want a metal printer right there.” Usually, it is said with a lot of confidence. And my first answer is almost always the same question: “What part are you going to make on it on a Tuesday afternoon in eighteen months?”
As a result, that question tends to stop the conversation for a minute. Not because people haven’t thought about additive manufacturing, but because most of them have been thinking about the machine instead of the work. After years of helping manufacturers select, install, and qualify industrial 3D printer equipment, I can tell you that the machine is rarely the thing that makes or breaks the investment. Instead, the parts, the people, the powder room, the post processing line, and the paperwork do.
So let me walk you through how I actually approach this with clients. In other words, not the brochure version, but the version where we talk about the mistakes that cost real money and the questions that save it.
Start With the Parts, Not the Printer
Every good decision about industrial 3D printer equipment that I have been part of started with a spreadsheet of parts, not a spreadsheet of printers.
Before you look at a single spec sheet, pull together a list of candidate parts. At first, I usually ask for somewhere between twenty and fifty. Then, for each one, I want to know the material, the rough size, the annual volume, the current cost, the current lead time, and what makes it painful today. For example, it could be a fixture that takes six weeks to come back from the machine shop. Or perhaps it is a spare part for a line that was installed in the nineties, and the supplier no longer exists. Sometimes it is a bracket that is five pieces welded together when it could be one.
Let the Patterns Guide You
Once that list exists, patterns show up fast. For instance, you might find that seventy percent of your opportunities are jigs, fixtures, and end of arm tooling in engineering plastics. That points you in a very different direction than a list full of stainless steel manifold blocks with internal cooling channels.
Still, I will be blunt here. If you cannot fill that list with parts that clearly benefit from additive, you are probably not ready to buy industrial 3D printer equipment. Instead, you might be ready to outsource a few builds through a service bureau and learn from them, which is a perfectly smart place to be. The Wohlers Report 2025 noted that while the overall AM industry grew 9.1 percent to about 21.9 billion dollars in 2024, system manufacturers saw a decline while service providers, software, and materials grew. Clearly, that tells you something. A lot of companies are choosing to buy parts before they buy machines, and plenty of them are right to.
Understand the Seven Process Families Before You Talk to Sales
The industry standard ISO/ASTM 52900 groups additive manufacturing into seven process categories: material extrusion, vat photopolymerization, powder bed fusion, material jetting, binder jetting, directed energy deposition, and sheet lamination. You do not need to become an expert in all seven, but you should know enough to recognize when a salesperson is steering you toward the process they happen to sell rather than the one your parts need.
Where Each Process Fits on the Shop Floor
With this in mind, here is how I explain the main options to a manufacturing team in plain terms.
Material extrusion (FDM or FFF): A heated nozzle lays down thermoplastic filament. Industrial versions handle materials like ABS, ASA, nylon, polycarbonate, carbon fiber reinforced nylon, and on the high end, PEEK and ULTEM. In practice, this is the workhorse for fixtures, gauges, and tooling. Parts are strong enough for a lot of shop use, but they are anisotropic, meaning they are weaker between layers than along them. Therefore, your engineers need to design with that in mind.
Vat photopolymerization (SLA and DLP): A light source cures liquid resin layer by layer. As a result, you get excellent surface finish and fine detail. It is great for molds, patterns, fluid handling prototypes, and small precise parts. The tradeoff is that resin parts can be more brittle, some materials are sensitive to UV exposure over time, and you have a wash and cure step that involves chemicals your EHS team will want to review.
Powder bed fusion, polymer (SLS and MJF): A laser or fusing agent and heat melt nylon powder in a bed. There are no support structures because the surrounding powder holds the part. Consequently, that makes it very efficient for batches of small, complex parts nested together in one build. If you want production runs of functional plastic components, this is often where I end up.
Metal Processes: Where the Stakes Go Up
Powder bed fusion, metal (LPBF or DMLS): A laser melts fine metal powder in an inert atmosphere. Generally, this is where you get dense, high performance parts in stainless, aluminum, titanium, nickel alloys, and tool steels. It is also where the complexity, facility requirements, and cost go up sharply.
Binder jetting: A print head deposits binder onto powder, and the green part is later sintered in a furnace. Metal binder jetting has real potential for higher volumes of smaller parts, but shrinkage during sintering has to be well understood and controlled.
Directed energy deposition (DED): A laser, electron beam, or arc melts wire or powder as it is deposited. Even so, it is useful for large parts, repair of worn components, and adding features to existing parts. Accuracy is lower, so plan for machining.
Material jetting and sheet lamination have their places too, but they come up less often in the facility projects I see.
Know the Difference Between a Printer and a Production Cell
In fact, this is the single biggest blind spot I run into with industrial 3D printer equipment. A client budgets for the printer and forgets they are really buying a cell.
For a metal powder bed fusion system, the cell might include a depowdering station, a sieving and powder recovery unit, a powder storage area with humidity control, an inert gas supply, a stress relief or heat treatment furnace, a wire EDM or band saw to remove parts from the build plate, CNC machining for critical surfaces, blasting or finishing equipment, and some form of inspection, often including CT scanning for internal features.
IMTS published a good piece on the hidden costs of additive manufacturing that lines up with what I see in the field. Specifically, they point to finishing, material handling, inspection, and qualification as the big four. Material handling in particular, meaning depowdering, recovery, sieving, storage, and dust control, can rival the cost of the printer itself. I have watched that happen more than once.
Even polymer systems have a cell behind them. For example, SLS needs a breakout station and media blasting. Similarly, SLA needs washing and curing stations and a way to manage used solvent. Likewise, industrial FDM needs support removal, which may mean a soluble support tank and a place to handle the wastewater.
Budget for the Whole Cell
When I build a budget with a client, I usually tell them to assume that the supporting equipment, facility work, and first year of operation will add a meaningful amount on top of the printer quote. In particular, for metal, it is common for that number to approach or exceed the machine price. If that number surprises you, it is much better to be surprised on paper than after the purchase order goes out.
Calculate the True Cost of Ownership
Let’s talk money, because the price of industrial 3D printer equipment is what the capital request committee will want to talk about.
Aniwaa put together a useful breakdown of total cost of ownership for metal 3D printing. According to them, end to end metal systems typically start around 100,000 dollars and often run well past 250,000. Metal powders like aluminum and stainless steel can exceed 100 dollars per kilogram, and titanium can reach around 300 dollars per kilogram. In addition, inert gas for powder bed systems can run into thousands or tens of thousands of dollars per year. On top of that, maintenance contracts commonly land in the tens of thousands annually. Finally, add software subscriptions, facility utilities, and the salary of someone who actually knows how to run the thing.
What Polymer Systems Cost
On the polymer side, the Formlabs guide gives a sense of the spread. Professional SLA systems start in the low thousands, industrial SLS systems begin around 30,000 dollars, and metal starts north of 100,000.
The Three Cost Buckets
When I build a cost model, I break it into three buckets.
Capital: Printer, supporting equipment, facility modifications, installation, and initial training.
Operating: Materials, gas, energy, consumables like build plates and recoater blades, maintenance contracts, software, and labor.
Hidden and quality costs: Failed builds, scrap, machine downtime, inspection, and the cost of qualifying parts and processes.
Weighing Cost Against Value
Then I compare that against what you currently spend on the parts in your candidate list, plus the value of things that are harder to put a number on, like shorter lead times, reduced inventory, and fewer line stoppages waiting on a replacement part. Above all, that last category is where additive often earns its keep. A 3D printed fixture that costs a bit more than a machined one but arrives in two days instead of five weeks can pay for itself in a single avoided downtime event.
One more note on utilization. A printer that runs twenty percent of the time is expensive, whereas one that runs eighty percent of the time starts to look very reasonable. Be honest with yourself about how many hours per week the machine will actually be printing, and do not assume you will hit full utilization in year one. In my experience, most facilities I work with take six to twelve months to build up a steady flow of work.
Match Build Volume and Throughput to Real Demand
With industrial 3D printer equipment, bigger is not always better. I have seen companies buy a large format machine because they had one or two big parts in mind, and then spend the next two years running small parts in a huge chamber. Unfortunately, that wastes powder, gas, time, and energy.
So, look at your part list again. What is the size distribution? If ninety percent of your parts fit in a 250 millimeter cube, a machine with that envelope might serve you well, and you can outsource the handful of larger parts. If you need production volumes, think about throughput in parts per week, not layer time on a brochure. Also, ask vendors for real benchmark builds using your geometry, not their showcase part.
For metal, multi laser systems can increase throughput significantly, but they also add calibration complexity where the laser fields overlap. Because of that, ask how the vendor handles stitching and how they verify it over time.
For polymer powder bed fusion, pay attention to packing density. After all, the ability to nest a lot of parts in three dimensions is one of the biggest economic advantages of SLS and MJF. As a result, a build that is packed well can bring the per part cost down dramatically.
Evaluate Materials and the Supply Chain Behind Them
Material choice drives almost everything downstream, so give it real attention.
First, is the material you need available and validated on the system? Some platforms are open, meaning you can use third party materials. In contrast, others are closed and require vendor supplied materials. Closed systems often give you more consistent results out of the box, but you pay for it and you are dependent on one supplier. Open systems give you flexibility and sometimes lower cost, but you take on more responsibility for developing and validating parameters.
Second, what does the data look like? Specifically, ask for material datasheets with tensile, elongation, and heat deflection data, and ask how the testing was done, in which build orientations, and with what post processing. Keep in mind that a datasheet value tested in the strongest orientation after heat treatment is not the value you will get from a part printed flat with no heat treatment.
Third, think about powder reuse. For instance, in polymer powder bed fusion, refresh rates, meaning how much fresh powder you have to mix with used powder, have a big impact on cost. In metal, powder reuse needs to be tracked carefully because chemistry and particle size can shift over many cycles. Therefore, your quality system should know which powder lot went into which build.
Plan the Facility Before the Machine Arrives
I have seen industrial 3D printer equipment worth 400,000 dollars sit crated for three months because nobody checked whether the floor could handle the load, or whether the building had the right power supply. So, do not let that be you.
Here is a short checklist I walk through with every facility.
Power: Many industrial systems need three phase power and dedicated circuits. Therefore, check voltage and amperage requirements early.
Floor and access: Confirm floor load ratings, door widths, and the path from the loading dock to the final spot.
Environment: Temperature and humidity control matter for both the printer and the materials. Resins and nylon powders are especially sensitive to humidity.
Gas: Metal systems need argon or nitrogen. Then decide between bulk tanks, cylinder banks, or a nitrogen generator, and plan the plumbing.
Ventilation and air quality: First of all, printing processes can release particles and vapors. NIOSH has published guidance on safer 3D printing, and while its 2024 guide was aimed at makerspaces, schools, and small businesses, the principles of local exhaust, enclosure, and good housekeeping apply even more strongly in an industrial setting.
Fire and explosion risk: Fine metal powders, especially aluminum and titanium, can be combustible. You need proper storage, grounding, inerting procedures, and a class D fire extinguisher, and your fire protection engineer and insurer should be involved from the start.
Space for the cell: Leave room for post processing, powder storage, inspection, and a clean spot for parts coming off the line.
Staffing and Skills Are Not Optional
Of course, a lot of vendors will tell you their industrial 3D printer equipment is easy to run. And to be fair, loading a job and pressing start is not hard. However, what is hard is knowing why a build failed, how to orient a part to reduce support and distortion, how to adjust parameters for a new geometry, and how to design parts that actually take advantage of additive.
At minimum, you want one person who owns the technology. On the metal side, I prefer to see someone with a materials or manufacturing engineering background, plus a technician who handles day to day operation and post processing. On the other hand, for polymer systems, a strong technician with design support from engineering can often carry it.
Also, budget for training, and not just the basic course the vendor includes. Design for additive manufacturing training for your engineers is one of the best investments you can make, because the biggest gains come from redesigning parts, not from printing existing designs.
I also recommend building relationships outside the company. For example, groups like America Makes, ASTM committee F42, and regional manufacturing extension partnerships offer training, standards work, and a network of people who have already solved the problem you are about to face.
Software, Data, and Integration
The printer is only as good as the workflow feeding it. First, look at the build preparation software. Is it vendor specific, or can you use third party tools? How does it handle orientation, support generation, nesting, and simulation?
For production environments, ask about machine monitoring and traceability. Can the system log sensor data for every layer, and can you connect it to your MES or ERP? If you are in a regulated industry, you will want that data for every part.
Cybersecurity deserves a mention too. After all, build files are intellectual property, and the machines are networked. For that reason, get your IT team involved early to set up segmentation and access controls.
Qualification and Quality Control
If you make parts for aerospace, defense, medical, or energy, this section may be the longest part of your project. That is because additive parts often need a qualified process, which means you prove the machine, the material, the parameters, and the post processing produce consistent results.
Even if you are not in a regulated industry, you need a quality plan. At the very least, that includes witness coupons in builds, dimensional inspection, regular calibration checks, powder testing, and clear documentation of what changed and when.
ASTM and ISO have been developing a large library of additive standards, and they are worth following. When I help a client choose industrial 3D printer equipment for a regulated application, I always ask the vendor which customers have already qualified parts on that system in that industry. Frankly, it is much easier to follow a path someone else has cleared.
How I Run a Vendor Evaluation
When a client is ready to buy industrial 3D printer equipment, here is the process I usually follow.
Shortlist based on process fit: Two to four systems that match the part list and material needs.
Benchmark builds: Send each vendor the same set of real parts, and then ask them to build, post process, and return them with inspection reports and build time data. Afterward, measure the parts yourself.
Site visits and reference calls: Ideally, visit a customer running the system in production, not just the vendor showroom. Also, ask references about uptime, service response time, and what surprised them.
Service and support: Ask where the nearest field service engineer is located, what the response time commitment is, and what spare parts are stocked locally.
Contract terms: Look at warranty, uptime guarantees, material restrictions, software licensing, and upgrade paths.
Total cost model: Finally, plug everything into the cost of ownership model we talked about.
Only then should you decide, and not before.
Buy, Lease, or Outsource?
This is a legitimate question, although there is no single right answer.
Outsourcing to a service bureau makes sense when demand is uncertain, when you need a process you cannot justify buying, or when you want to learn before committing. Meanwhile, leasing can help spread cost and reduce the risk of being stuck with aging technology. Buying makes sense when you have steady, predictable demand, parts you want to keep in house for IP or lead time reasons, and a team ready to run the equipment.
In reality, many of my clients do a mix. They buy a polymer system for fixtures and tooling, which pays back quickly, and outsource metal parts until the volume justifies bringing that in house.
Common Mistakes I Keep Seeing
To wrap up, let me close the main discussion with the mistakes that come up again and again.
Buying the machine before identifying the parts. Underestimating post processing. Treating the printer like a copier and not assigning an owner. Choosing the biggest machine on the market for a handful of large parts. Skipping facility and safety planning. Expecting existing designs to become cheaper just because they are printed. And assuming the first year will look like the fifth year.
Admittedly, none of these are fatal on their own. Together, they are how a promising project ends up as an expensive machine covered with a tarp.
Final Thoughts
Choosing industrial 3D printer equipment is not really a technology decision. Rather, it is a manufacturing strategy decision that happens to involve some very interesting technology. If you start with the parts, understand the full production cell, model the real cost, plan the facility, invest in your people, and take qualification seriously, you will make a good decision. It might even be a decision not to buy yet, and that is okay.
The Wohlers Report 2026 values the additive market at around 24.2 billion dollars, and it is clear the technology is maturing. But maturity in the industry does not mean maturity in your facility. That part is up to you and your team.
If you are in the middle of this decision, take a step back and ask the question I ask every client. What part are you going to make on it on a Tuesday afternoon in eighteen months? If you can answer that clearly, you are already ahead of most.
Frequently Asked Questions
What is industrial 3D printer equipment?
It is the full set of additive manufacturing systems used in a production setting, including the printer itself plus supporting equipment for material handling, post processing, and inspection. Unlike desktop units, industrial systems are built for repeatability, larger build volumes, engineering materials, and continuous operation. Formlabs: How to Choose an Industrial 3D Printer
How much does industrial 3D printer equipment cost?
Generally, prices vary widely by process. Professional resin systems start in the low thousands, industrial SLS systems start around 30,000 dollars, and end to end metal systems usually start around 100,000 dollars and often exceed 250,000. Supporting equipment and facility work can add significantly to that. Aniwaa: Total Cost of Ownership for Metal 3D Printing
What are the hidden costs of additive manufacturing?
The biggest ones are finishing and post processing, material handling, inspection, and qualification or certification. In fact, for powder systems, material handling equipment alone can rival the printer’s price. IMTS: Hidden Costs of Additive Manufacturing
Which 3D printing process is best for manufacturing?
Ultimately, it depends on your parts. FDM suits fixtures and tooling, SLA suits precise parts and molds, SLS and MJF suit batches of functional plastic parts, and metal powder bed fusion suits complex, high performance metal components. Wohlers Associates: The Seven AM Processes
Is 3D printing safe in a factory environment?
It can be, with proper controls. Printing can release particles and vapors, and metal powders can pose fire and explosion risks. Therefore, ventilation, enclosure, proper storage, and trained staff are essential. CDC NIOSH: 3D Printing (Additive Manufacturing)
Should we buy a printer or use a service bureau?
If demand is uncertain or you need a process you cannot justify owning, a service bureau is a smart way to start. Buying makes more sense with steady demand, IP concerns, and a team ready to run the equipment. In addition, industry data shows service providers continuing to grow. Wohlers Report 2025 shows 9.1% AM industry growth
How big is the additive manufacturing market?
The Wohlers Report 2026 values the global additive manufacturing market at 24.2 billion dollars. ASTM: Wohlers Report 2026
References
ASTM International, “New Wohlers Report 2026 Values Additive Manufacturing Market at $24.2B,” https://www.astm.org/news/press-releases/wohlers-report-2026
Wohlers Associates, “Wohlers Report 2025 shows 9.1% AM industry growth,” https://wohlersassociates.com/news/wohlers-report-2025-shows-9-1-am-industry-growth/
Wohlers Associates, “The Seven AM Processes,” https://wohlersassociates.com/terminology-and-definitions/the-seven-am-processes/
Formlabs, “How to Choose an Industrial 3D Printer,” https://formlabs.com/blog/industrial-3d-printer/
Aniwaa. “What’s the total cost of ownership for metal 3D printing?” https://www.aniwaa.com/insight/3d-printers/total-metal-3d-printing-cost/
IMTS, “Hidden Costs of Additive Manufacturing,” https://www.imts.com/read/article-details/Hidden-Costs-of-Additive-Manufacturing/2399/type/Read/1/tab/all-articles?page=1
CDC NIOSH, “3D Printing (Additive Manufacturing),” https://www.cdc.gov/niosh/manufacturing/additive/index.html
CDC NIOSH, “Approaches to Safe 3D Printing: A guide for makerspace users, schools, libraries, and small businesses,” https://www.cdc.gov/niosh/publications/numbered/2024-103.html
Metal AM, “Wohlers Report 2025 shows global additive manufacturing industry growth over 9%,” https://www.metal-am.com/wohlers-report-2025-shows-global-additive-manufacturing-industry-growth-over-9/